VanguardEdge
Get a Quote
Latest

From raw material markets to the dye bath.

Guide
2026.10  ·  Guide

Reading a yarn count: what NM, Ne and tex actually mean

Read more
A yarn count is simply a way of describing how thick a yarn is — but the industry uses at least three different systems, and mixing them up is one of the most common causes of a mis-quoted order. — NM (metric count) tells you how many 1,000-metre lengths weigh 1 kg. A higher NM means a finer yarn, so 2.6 NM is thin and 0.14 NM is extremely thick. Most of our hand knitting range sits between 0.1 NM and 2 NM — the super-bulky end used for arm knitting and one-ball blankets. — Ne (English cotton count) works on 840-yard hanks per pound, which is why the numbers look different from NM for the same yarn. A yarn quoted as 2.5 Ne is not the same as 2.5 NM. — Tex works the opposite way: it measures grams per 1,000 metres, so a higher tex number means a thicker yarn. Tex is common in technical and industrial specifications where weight per length matters more than knitting gauge. When you see a specification like "0.14 NM / 2 cm", the two numbers describe different things: the NM value is the count, and 2 cm is the measured diameter of the yarn. Both are useful — count for ordering, diameter for estimating how a stitch will look. The practical rule when comparing suppliers: always confirm which system is being used, and always ask for the weight and length per ball or cone rather than the count alone. Weight and length are unambiguous no matter which system the supplier prefers.
Auxiliaries
2026.09  ·  Auxiliaries

Formaldehyde-free fixing agents move from option to default

Read more
For years, formaldehyde-free fixing agents sat in the "nice to have" column. That has changed. With ZDHC MRSL updates and tightening OEKO-TEX limits across major export markets, non-formaldehyde fixatives are now the default choice for reactive-dyed cellulosic fabrics destined for Europe and North America. The chemistry behind it matters. A conventional fixing agent works by forming a cross-linked film over the dyed fibre, which locks in the dye but can release formaldehyde over time or under heat. Modern non-formaldehyde alternatives use cationic polymers that achieve comparable wet and rub fastness without that trade-off. — What to check when evaluating a fixing agent. — Wet fastness. The primary function. A useful benchmark is one full point improvement in the wash test after treatment. — Shade change. Some fixatives shift the shade slightly, particularly on turquoise and bright red. Always run a lab dip comparison rather than relying on the TDS. — Hand-feel impact. Cationic fixatives can stiffen the fabric if over-dosed. Check the recommended range carefully. — Documentation. For export programmes the paperwork is as important as the chemistry. Ask for the ZDHC conformance level and a current OEKO-TEX ECO PASSPORT if your buyer requires it. Because fixing is usually the last wet process before drying, it is also the last chance to correct a fastness problem. Getting it right at this stage is far cheaper than re-processing.
Auxiliaries
2026.07  ·  Auxiliaries

Yarn packaging explained: cones, cheeses, hanks and balls

Read more
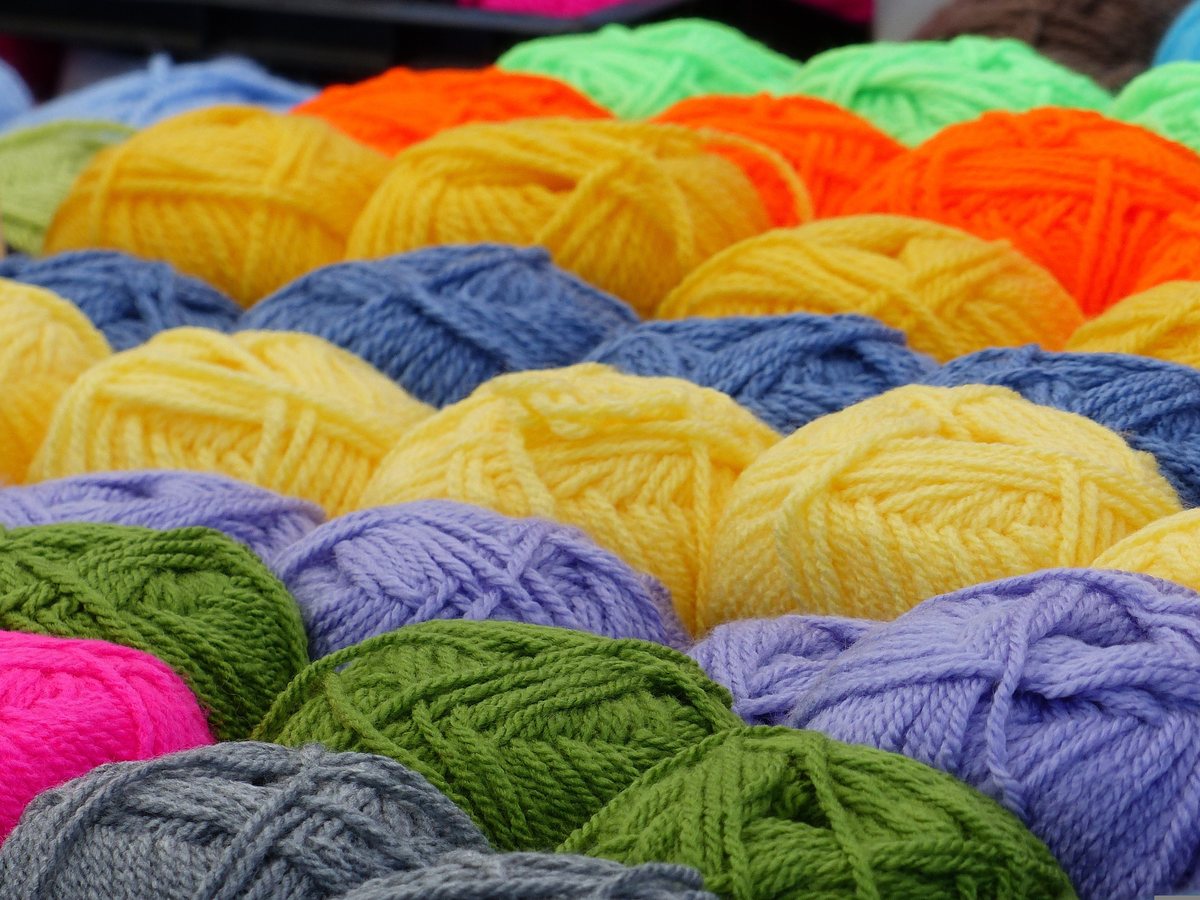
The same yarn can arrive in completely different packaging depending on what it is destined for — and choosing the wrong format causes problems on the machine. — Cones and cheeses. Wound onto a tapered or cylindrical core, these are the standard package for machine knitting and weaving. A cheese is a parallel-wound package; a cone is tapered so the yarn unwinds from the side without snagging. Both allow continuous feeding at speed, which is why they dominate industrial supply. — Hanks. A hank is a loose loop of yarn, usually tied in several places. Hanks are what you get when yarn needs to be dyed after spinning, because dye penetrates a loose hank far more evenly than a dense package. They are also used for hand-dyeing and for yarns that would be crushed by tight winding. — Balls. Balls are the retail format: wound so that the yarn pulls from the centre or the outside without tangling. Hand knitting balls are usually 50 g to 226 g, and the ball weight is what most consumers compare when they shop. — Pallets and cartons. For export, the packaging question moves up a level: how many balls per polybag, how many bags per carton, and whether the carton is palletised. Vacuum compression is common for bulky hand knitting yarn because it reduces shipping volume substantially without damaging the fibre. Practical advice: if you are sourcing for machine knitting, specify cone or cheese and confirm the taper and core diameter. If you are sourcing for retail, specify ball weight, bag count and carton count — and ask for a sample of the actual packing, not just the yarn. The packing is often where a shipment fails inspection, not the yarn itself.
Auxiliaries
2026.04  ·  Auxiliaries

Water-saving dyeing: what dyehouses are actually asking for

Read more
Wastewater treatment costs have risen faster than most other operating expenses in the dyehouse over the past three years. The result is a clear shift in what converters ask for: not "the cheapest auxiliary", but "the auxiliary that lets us use less water". There are three practical routes to cutting water in the dye bath, and each has implications for the chemistry: — Shorter liquors. Reducing the liquor ratio from 1:12 to 1:8 cuts water per batch substantially, but it also reduces the dilution buffer for the chemicals. Products that disperse easily and work at lower concentrations become essential, particularly leveling agents. — Fewer rinse steps. Soaping agents that rinse out faster allow one rinse bath to be eliminated. The key metric is not the initial soaping performance but how completely the auxiliaries themselves wash out, since residues cause fastness problems downstream. — Combined processes. Combining scouring and bleaching, or dyeing and soaping, saves both water and time — but requires auxiliaries that are compatible under the combined conditions, and the compatibility window is narrower. In practice, most dyehouses we work with combine all three approaches, starting with the highest-volume recipes. The savings are usually measured first in water and energy, then in reduced effluent load — which is often where the larger long-term cost sits.
Yarn
2026.01  ·  Yarn

Polyester feedstock: what PTA and MEG movements mean for yarn prices

Read more
Almost all polyester yarn starts with two chemicals: PTA (purified terephthalic acid) and MEG (monoethylene glycol). Both are derived from crude oil, and both move with it — but not always in step, and not always in the direction buyers expect. What actually drives the price of a polyester yarn quote: — Feedstock spread. PTA and MEG production margins expand and contract independently of crude. A period of stable crude can still see feedstock prices rise if plant utilisation drops. — Plant maintenance seasons. Scheduled turnarounds at major PTA plants in Asia remove supply temporarily. Buyers who track these windows can often time their purchasing better. — Regional supply. Chinese domestic pricing and export pricing do not always move together, particularly when export demand is strong. — Exchange rates. For an export buyer, the RMB/USD rate can move a quoted price as much as the underlying feedstock. The practical takeaway: yarn quotes typically carry a short validity window because spinners cannot hedge feedstock indefinitely. In a rising market, locking raw material earlier is usually cheaper than waiting for a better price that does not arrive. In a falling market, the reverse is true — which is why we quote with a stated validity rather than an open-ended price.
Guide
2025.12  ·  Guide

Where auxiliaries sit in the wet-processing line

Read more
Auxiliaries are usually sold by function — refining, leveling, softening — but it helps to understand where in the process each one sits, because that determines what a problem looks like when something goes wrong. A typical cotton knit passes through four chemical stages: — 1. Pretreatment. Refining agents remove natural waxes, pectin and oils. Degreasing agents handle added oil from spinning. Penetrating agents ensure the fibre wets evenly. Chelating dispersants capture metal ions from water and fibre so they cannot interfere later. If you see uneven dyeing, the cause is often here, not in the dye bath. — 2. Dyeing. Leveling agents control how evenly dye is taken up. Soaping agents remove unfixed dye after the dye cycle. Reduction clearing removes disperse dye residue from polyester. Anticreasing agents prevent crease marks during winch or jet processing. — 3. Finishing. Softeners, hydrophilic softeners, smoothing agents and bulking agents modify hand-feel and surface. This is where the fabric gains its "sellable" character. — 4. Functional finishing. Antistatic and moisture-wicking agents add a specific performance property on top of the base finish. The diagnostic value of knowing the stage: a fastness complaint points at dyeing or fixing; a hand-feel complaint points at finishing; a patchy appearance points at pretreatment. Starting from the right stage saves a lot of trial and error.
Yarn
2025.09  ·  Yarn

Recycled polyester (rPET) moves from niche to mainstream

Read more
Three years ago, recycled polyester was something buyers asked about at the end of a meeting. Now it is often the first question. The change has been driven by brand-level sustainability targets, but the technical story has also improved considerably. What has changed on the supply side: — Feedstock quality. Food-grade rPET flake supply has become more reliable, and the consistency of the input material has improved. This matters more than it sounds — inconsistent feedstock is the main cause of spinning breaks in recycled yarn. — Spinning performance. Modern rPET is much closer to virgin polyester on the spinning floor. Tenacity and elongation have improved to the point where most standard constructions can run recycled content without adjusting machine settings. What still requires attention: — Colour consistency. This remains the main trade-off, particularly in dark shades and deep dyed colours, where batch-to-batch variation is wider than with virgin fibre. Light and mid-tones are far less affected. — Certification. If your buyer needs traceability, confirm the chain-of-custody documentation (GRS or equivalent) before committing to a delivery date. — Price premium. rPET still carries a premium over virgin in most markets, though the gap has narrowed. We can now offer recycled blends on selected constructions. Availability varies by count and colour, so it is worth asking early in the enquiry.
Guide
2025.06  ·  Guide

Why space-dyed yarn looks different in every ball

Read more
Space-dyed yarn is built on a simple idea: a white base with regular colour segments, typically 2–3 cm long, repeated along the length. The effect in finished work is anything but simple. How it is actually made: the yarn is wound into a hank and dye is applied to sections of the hank, leaving the rest white. Because the segments repeat on a fixed interval determined by the winding, the colour cycle is regular — but the point in the cycle where a given ball starts is not. That is why two balls from the same production lot can look noticeably different when you begin working with them. It is not a defect; it is a consequence of how the yarn is wound and dyed. In a finished blanket, the effect reads as organic variation rather than mechanical striping — which is precisely what most makers are looking for. Practical points when working with space-dyed yarn: — Alternate balls. Working from two balls alternately evens out the colour distribution across the piece. — Expect pooling. In wide panels, the colour segments can pool into diagonal bands. Some makers plan for this deliberately; others break it up by changing needle size slightly. — Order enough at once. Because the segment pattern is set during winding, we recommend ordering the full quantity for a project in a single lot. If you need a perfectly uniform colour, a solid-dyed yarn is the right choice. Space-dyeing is specifically for makers who want variation.
Guide
2025.03  ·  Guide

What is chenille yarn? A beginner guide to plush yarns

Read more
Chenille yarn takes its name from the French word for caterpillar, which describes its appearance well: a soft, fuzzy pile that stands out from a central core, giving a rounded, plush profile. How it is made: short fibres (the pile) are held between two tightly twisted core strands. Because the pile is gripped rather than spun in, it stands outward along the whole length of the yarn — which is what produces the velvety surface. The construction also explains why chenille is so thick relative to its weight. Two properties matter most when choosing a chenille: — Pile density. A denser pile sheds less fibre, holds its appearance after washing, and feels more substantial. Low-density chenille can look thin and shed noticeably, particularly in dark colours on light backgrounds. — Core strength. The core is what carries the tensile load. If the core strand is too thin, the yarn snaps under tension — most visibly during arm knitting, where the whole blanket weight hangs from a single working loop. A thicker core allows a looser, faster technique without breakage. What chenille is good for: blankets, cushions, cat beds, decorative pillows and home textiles — anywhere softness matters more than stitch definition. Chenille hides stitch patterns, which makes it forgiving for beginners but less suited to lace or cable work. Care: because the pile is mechanically held, chenille generally benefits from gentle washing and low-heat drying. Most of our jumbo chenille is machine washable when the finished piece follows the recommended gauge.
Guide
2025.02  ·  Guide

Colour fastness explained: wash, rub, light and perspiration

Read more
Fastness ratings tell you how a dyed fabric behaves in real use. They are usually quoted on a 1–5 scale (sometimes 1–8 for light fastness), where higher is better. Understanding which rating applies to which situation prevents a lot of avoidable disputes. — Wash fastness covers colour loss and staining during laundering. It matters on anything that will be washed repeatedly — apparel, towels, bedding. A rating of 4 or above is generally expected for export apparel. — Rub fastness is measured dry and wet. Wet rub is almost always lower, and is the one that matters on dark, saturated shades — particularly reactive blacks and navy blues. Poor wet rub is often a fixing problem rather than a dyeing problem. — Light fastness measures resistance to fading under exposure. It is critical for curtains, upholstery, outdoor textiles and anything displayed near a window. Ratings here use a wider scale, and a low rating on a furnishing fabric is a serious issue. — Perspiration fastness covers both colour change and staining of adjacent fabric when exposed to acidic and alkaline sweat. It is essential for anything worn against the skin, and is often specified separately for the two pH conditions. The important point is that a fabric can score well on one standard and poorly on another. Cotton reactive dyeing that achieves excellent wash fastness can still have mediocre light fastness. So the correct question is never "is this fast?" but "fast to what, under which standard?" Always confirm which standard your buyer is actually specifying — ISO, AATCC and GB test methods do not always produce identical numbers for the same fabric.

Have a question about a specific product?

Send us your specification and we will come back with technical data, samples and pricing.